

Transforming end-of-life tyres into virgin-grade recovered Carbon Black (rCB) is no longer a theoretical ambition, it is proven industrial engineering.
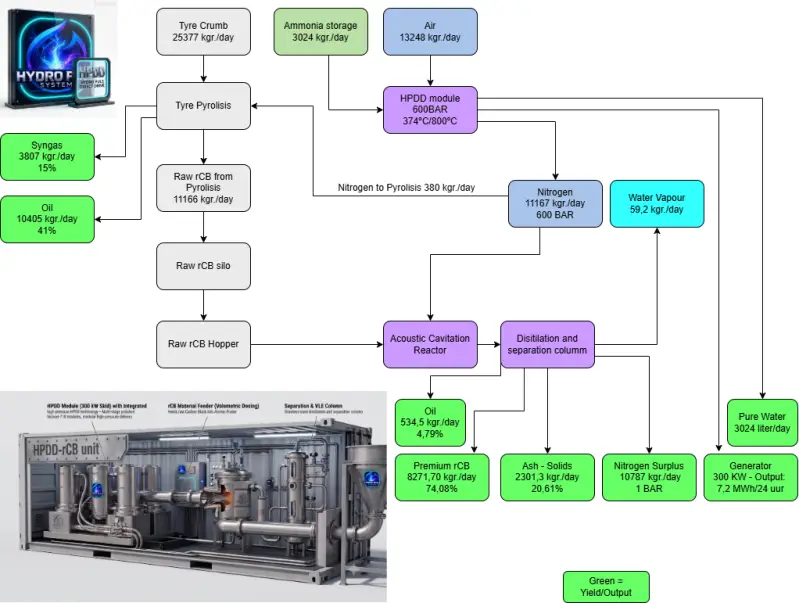
This exact process architecture and mass-balance flow diagram was engineered specifically for an industrial client in Ontario, Canada. It integrates the direct fluidic power of Hydro Puls Direct-Drive (HPDD) with the Acoustic Cavitation Reactor into a compact, containerized skid deployment.
The Challenge in Ontario:
Conventional tyre pyrolysis produces an unrefined, ash-heavy char. Without high-precision de-agglomeration and mineral de-ashing, this material fails to meet the strict technical specifications demanded by North American tier-one tyre and polymer manufacturers.
The Tailored HPDD Solution (Daily Input: 25,377 kg Tyre Crumb):
1. Integrated Fluidic Power & Inert Gas Core:
- The HPDD module combines atmospheric air (13,248 kg/day) and stored ammonia (3,024 kg/day) to produce a 600-BAR nitrogen stream (11,167 kg/day at 374 °C / 800 °C).
- Simultaneously, it supplies 300 kW of continuous baseload generation (7.2 MWh per 24 hours) and 3,024 liters/day of pure process water.
- 380 kg/day of hot nitrogen is diverted directly to blanket the pyrolysis reactor, eliminating external inert gas generation costs.
2. Primary Pyrolysis Separation:
- Syngas: 3,807 kg/day (15%)
- Pyrolysis Oil: 10,405 kg/day (41%)
- Raw rCB Char: 11,166 kg/day, routed straight to the dosing hopper and feed unit.
3. Cavitation Refining & Supercritical Separation:
The raw char is injected into the Acoustic Cavitation Reactor alongside the 600-bar nitrogen stream. Supersonic shockwaves shatter agglomerates in-flight down to a narrow sub-micron distribution (d50 < 1.0 µm) while stripping surface inorganics, with zero mechanical jet-milling wear.
The downstream separation and VLE column isolates high-value output streams:
- Premium rCB: 8,271.70 kg/day (74.08% yield), fully prepared for high-specification compounding
- Separated Ash/Solids: 2,301.30 kg/day (20.61%)
- Recovered Secondary Oil: 534.50 kg/day (4.79%)
- Clean Nitrogen Surplus: 10,787 kg/day at 1 BAR
A plug-and-play modular skid that delivers maximum circular value, on-site energy generation, and zero process emissions for our client in Ontario.
#CircularEconomy #RecoveredCarbonBlack #rCB #TyreRecycling #CleanTech #ProcessEngineering #HPDD #AcousticCavitation #Decarbonization #OntarioIndustry #WasteToValue