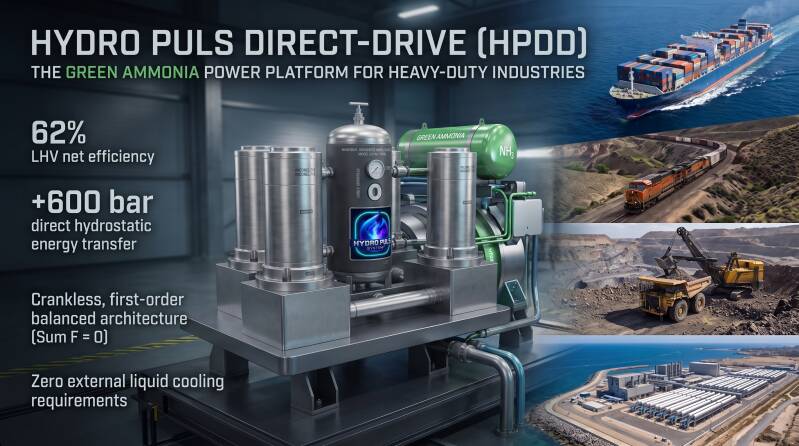
Two Revolutionary Technologies. One Autonomous Platform.

Modern industry demands more than incremental efficiency, it requires radical transformation. Hydro Puls Systems has developed two complementary technological pillars engineered to eliminate mechanical friction, prevent reactor fouling, and maximize unit economics across global energy, manufacturing, and environmental sectors.

The Future of Energy & Material Processing

Powerful. Clean. Autonomous.

Hydro Puls Systems redefines heavy industry with a software-defined hardware core. By replacing friction-heavy, high-maintenance machinery with advanced fluid kinetics and zero-wear architecture, we turn energy conversion and material processing into bankable, highly profitable assets.

Explore HPDD (Hydro Puls Direct Drive)

⚙️ Hydro Puls Direct-Drive (HPDD)

Zero-Emission Industrial Process & Fluid Platform


Hydro Puls Systems commercializes the Hydro Puls Direct-Drive (HPDD) platform: +600 bar linear hydrostatic power and Acoustic Cavitation Reactors (ACR) achieving 63% net efficiency without steam, chemicals, CO2, or NOx.

Hydro Puls Direct-Drive: The Autonomous Energy & Industrial Process Core

Where industrial physics becomes a constant.

Hydro Puls Systems redefines industrial thermodynamics through the Hydro Puls Direct-Drive (HPDD) platform. HPDD is not an internal combustion engine, nor is it a conventional hydraulic pump. It is a new class of direct-drive linear hydrostatic power and acoustic processing core, engineered to eliminate fossil steam boilers, parasitic friction, and hazardous chemical processing across heavy industry.

By operating with four pistons in rigid opposition (two pairs) floating on a 5-micron nitrogen clearance interface, HPDD completely bypasses crankshaft mechanics, side-loads, and wear-prone seals. Delivering continuous, pulsation-optimized work at up to +600 bar with a 63% net system efficiency, HPDD decouples power generation from driven load variations—operating permanently in its thermodynamic sweet spot.

The Breakthrough: Acoustic Cavitation Reactor (ACR) at +600 Bar & 374 °C

The decisive technological differentiator of the HPDD platform is the direct integration of the Acoustic Cavitation Reactor (ACR) driven by a closed-loop nitrogen cycle at 600 bar and 374 °C.

In conventional chemistry, acoustic cavitation is physically constrained by low ambient pressure. Inside HPDD's closed, ultra-dense nitrogen environment, the physics transform:

• Extreme Sonochemical Energy: Cavitation bubble collapse energy scales directly with ambient hydrostatic pressure. At +600 bar, localized acoustic shockwaves tear long-chain molecular polymers apart purely mechanically.
• 100% Chemical-Free Processing: Eliminates the requirement for acidulation, caustic cracking agents, toxic solvents, or consumable catalysts.
• Zero Emissions (Zero CO2, Zero NOx): Pure nitrogen serves as the hermetically sealed thermodynamic medium. Without atmospheric combustion, thermal NOx and direct CO2 emissions are fundamentally zero.
• Rapid Reaction Kinetics: Reaction and separation times drop from hours to milliseconds, slashing industrial primary energy consumption.

Four Fundamental Engineering Pillars

1. Zero-Friction Gas-Curtain Interface:
The transduction pistons float within a high-pressure nitrogen labyrinth seal maintaining a 25-micron clearance gap. With zero metal-to-metal contact, mechanical friction losses drop to just 1.5%, a fraction of the 12% lost in classical crankshaft systems.

2. Thermal Stabilization at 230 °C (ITS):
Through an unpressurized Siloxane-filled Internal Thermal System (ITS) jacket, core components maintain a steady 230 °C operating baseline. At this exact temperature, precision Inconel cylinder borings and pistons expand by 109 µm to self-seal operating tolerances without mechanical rings.

3. Opposed-Piston Mass Balance (2 Pairs):
Two pairs of direct-opposed pistons cancel dynamic vibration and eliminate mechanical side-loads. Energy transfers via bulk-modulus fluid dynamics directly to the working fluid, cutting parasitic losses to 2.5%.

4. Scalable High-Frequency Architecture:
Running at a rock-solid master frequency of 100 Hz, with a validated roadmap to 200 Hz / 160 kW per module, the platform scales linearly to meet commercial industrial throughput.

Core Commercial Deployments

• Heavy Residue & Glycerin Pitch Valorization:
On-site, continuous upgrading of oleochemical and biodiesel waste streams (such as 1,000 ton/month glycerin pitch) into commercial-grade 80%+ crude glycerin and dry mineral fertilizers without acidulation or secondary effluents.

• Decarbonized Industrial Utilities (HPDD-NEXUS):
Modular, containerized replacements or enhancers for steam turbines and industrial boiler loops. Delivers responsive thermal and hydraulic work with zero partial-load degradation.

• Industrial Desalination & High-Pressure Fluid Handling:
Purely mechanical phase splitting, dewatering, and salt crystallization for aggressive industrial brines and zero-liquid-discharge (ZLD) requirements.

• Ultra-Class Heavy Machinery Retrofitting:
Compact, high-power-density linear direct hydraulics for off-highway, mining, and maritime applications ready for hydrogen and ammonia power loops.

Autonomous. Chemical-Free. Zero-Emission.
Hydro Puls Systems delivers containerized, plug-and-play process skids that convert industrial liabilities into immediate power

1. Hydro Puls Direct-Drive (HPDD)

The Autonomous Process & Energy Core

The Hydro Puls Direct-Drive (HPDD) platform replaces legacy crankshafts, high-wear seals, and parasitic mechanical couplings with a frictionless, opposed-piston linear direct-drive matrix.

Operating under a strict 230 °C wall isotherm with precise 109 µm Inconel thermal expansion and a 25-micron gas interface, the HPDD core eliminates metal-to-metal wear and gas blow-by while delivering +600 bar continuous hydrostatic work at 63% net efficiency.

Coupled with the Acoustic Cavitation Reactor (ACR), it unlocks 100% chemical-free, zero-emission processing for heavy industrial waste, biofuel valorization, and decarbonized thermal utilities.

Primary Applications: Chemical-Free Residue Valorization, Industrial Decarbonization, Zero-Emission Fluid Power.


Discover The: Acoustic Cavitation Reactor (ACR)

🔬 The HPDD Acoustic Cavitation Reactor

In-Flight Process Intensification & Material Upgrading

Industrial material processing, chemical conversion, and waste remediation have historically been constrained by physical contact. Traditional reactors, grinders, and calciners suffer from severe mechanical wear, wall coking, thermal degradation, and heavy equipment fouling.

The HPDD Acoustic Cavitation Reactor eliminates these failure points by executing multi-phase physical kinetics and chemical transformations completely in-flight, suspended in mid-air, before material can ever touch or foul an internal reactor wall.

How In-Flight Processing Works

The Acoustic Cavitation Reactor leverages the extreme fluid dynamics generated by the HPDD direct-drive core to achieve rapid, non-contact material destruction and restructuring:

  1. Supersonic Shockwave Generation:

    Driven by an oxygen-free, supercritical Nitrogen carrier loop operating at 600 BAR and 850°C, the system accelerates fluid flows past Mach 2.5 through custom ceramic De Laval nozzle arrays. This generates high-frequency acoustic decompression shockwaves.

  2. Mid-Air Flash-Shattering:

    Incoming feedstocks, whether dense slurries, toxic organics, or coarse char, are subjected to these acoustic shockwaves. Within milliseconds, rigid matrices (such as silicates, iron oxides, and carbon lattices) are flash-shattered in suspension into uniform, dry sub-micron powders ().

  3. Density Decoupling & Pure Extraction:

    Downstream vertical convective separation columns operate under strict Supercritical Vapor-Liquid Equilibrium (VLE) parameters (e.g., 230 BAR / 330°C). This forces an immediate non-equilibrium density decoupling: pure distilled process water condenses out of the top for 100% closed-loop factory reuse, while dry, fully neutralized high-value minerals drop out of the bottom under an exact mass balance ().

Key Environmental & Commercial Capabilities

  • 🧪 PFAS & Toxic Contaminant Destruction: Completely breaks down forever chemicals, hazardous organics, and complex industrial waste streams at the molecular level without toxic secondary emissions.

  • 🌑 Biochar to ASTM-Grade Carbon Black: Converts low-margin pyrolytic char and biochar into ultra-pure, high-value recovered Carbon Black (rCB) for tire, polymer, and advanced manufacturing markets.

  • 🏗️ Zero-Fouling Calcination (Cement 2.0): Replaces legacy calcination rotary kilns with instantaneous mid-air thermal activation, slashing energy overhead and eliminating mechanical wear.

  • ⛏️ Red Mud & Strategic Mineral Recovery: Processes harsh alkaline bauxite residue mid-air without wall coking, recovering neutralized iron, titanium, strategic rare-earth oxides, and pure water.

Core Advantages

  • 🟢 Zero Reactor Fouling & Coking: Because processing occurs in-flight, feedstocks never adhere to or degrade internal metallic surfaces.

  • 🟢 No Grinding Media or Moving Parts: Cuts out high-wear mechanical crushers, mills, and rotating shafts, dramatically lowering maintenance CAPEX/OPEX.

  • 🟢 Software-Defined Precision: Real-time digital controls dynamically adjust shockwave frequency and pressure ratios to adapt to varying feedstock moisture or composition instantly.

  • 🟢 100% Closed-Loop Efficiency: Zero waste discharge, native heat recovery, and complete water recycling back into the process.

2. The HPDD Acoustic Cavitation Reactor (ACR)

In-Flight Process Intensification & Material Upgrading

The Acoustic Cavitation Reactor solves the historic bottleneck of industrial processing: reactor fouling, coking, and mechanical degradation. By executing multi-phase reactions completely in-flight (mid-air in suspension), feedstocks never touch or foul internal reactor walls.

Utilizing a supersonic nitrogen carrier loop at 600 bar and 850°C, custom De Laval nozzle arrays generate high-frequency acoustic decompression shockwaves (past Mach 2.5). Raw materials and complex waste streams are flash-shattered within milliseconds into uniform, dry sub-micron powders.

  • Primary Applications: Biochar & Pyrolysis Upgrading, Zero-Liquid Discharge (ZLD) Water, Cement 2.0 Calcination.

Grounded in First-Principles Science & Institutional Rigor

Our technology isn't built in isolation. Guided by the scientific leadership of Prof. Dr. Mohamed Amin and developed in collaboration with global academic institutions, research centers, and EPCM partners, the HPDD platform is engineered to satisfy the most rigid underwriting standards of Tier-1 energy and infrastructure investors.

  • Globally Patented: Protected multi-physics architecture and mechanical designs.
  • Validated Unit Economics: Proven low OPEX (~0.72 kWh/m³) and zero-degradation hardware nodes.
  • Field-Ready Deployment: Built to transition seamlessly from validated modeling to continuous real-world operation.

Ready to Upgrade Your Industrial Infrastructure?

Whether you are looking to retrofit existing assets, eliminate environmental liabilities, or deploy autonomous energy nodes, Hydro Puls Systems provides the complete technical and economic framework.

NEWS

Decentralized Ammonia

Conventional ammonia production relies on massive, centralized Haber-Bosch plants fed by fossil natural gas (steam methane reforming), generating heavy CO2 emissions and requiring complex cryogenic transport to reach regional industrial and agricultural users.

Read more »

Direct oil from tyres

Instead of selling steel- and fiber-free rubber chips (5–25 mm) at commodity prices, or building high-maintenance 500 °C rotary-kiln pyrolysis plants, our modular HPDD + ACR + VCD platform converts rubber chips directly into clean fuel oil and high-grade rCB at ≤ 230 °C:

Read more »

Palm Oil Rafinage

Mild, Closed-Loop Palm Oil Refining (CPO & CPKO)Upgrade crude palm oil into export-grade RBD palm oil without heavy chemical degumming, high-temperature thermal degradation, cooling towers, or stack emissions.

Read more »

rCB and Ammonia production

Many tyre pyrolysis operators face two major bottlenecks: unstable grid power (forcing expensive Solar + short-duration battery setups) and under-monetized outputs, crude Tyre Pyrolysis Oil (TPO) and low-grade raw char.

Read more »

Coal to Ammonia

Conventional Coal-to-Liquids plants suffer from massive water consumption, heavy CAPEX, and downstream CO2 emissions. Pairing Coal-to-Ammonia with Hydro Puls Direct-Drive (HPDD) changes everything:

Read more »