Decentralized Ammonia (NH3) Production from Waste Tyre Rubber
Turn end-of-life tyre chips and non-condensable off-gases into high-purity ammonia, recovered Carbon Black (rCB), 24/7 off-grid power, and potable water—without natural gas reforming or external grid power.
Conventional ammonia production relies on massive, centralized Haber-Bosch plants fed by fossil natural gas (steam methane reforming), generating heavy CO2 emissions and requiring complex cryogenic transport to reach regional industrial and agricultural users.
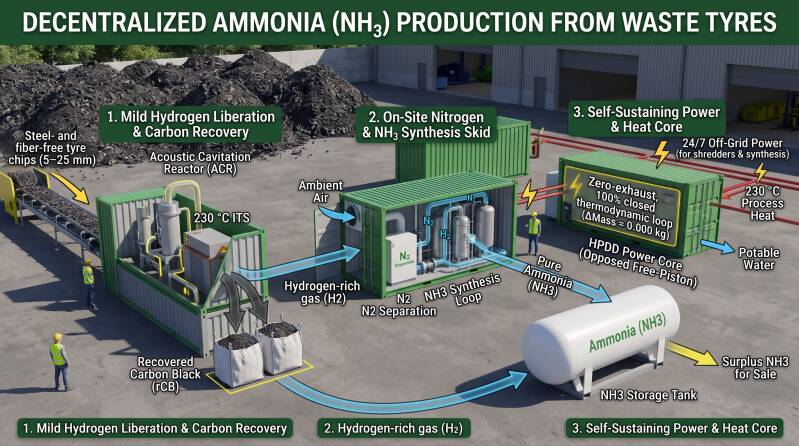
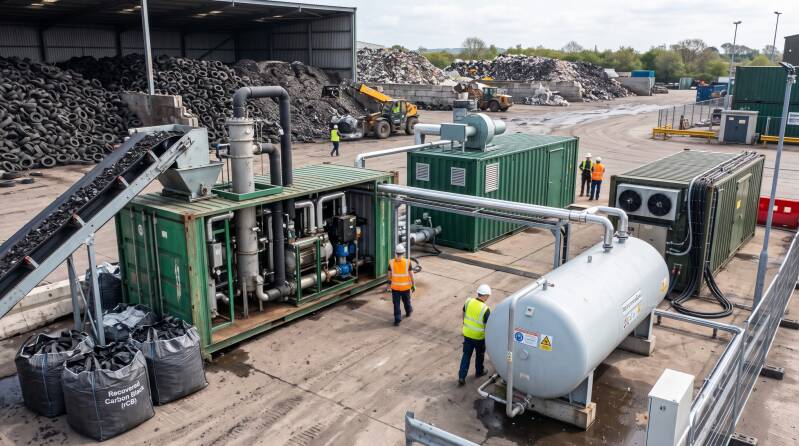
Hydro Puls Direct-Drive Systems (HPDD) turns mechanical tyre recycling sites into self-sustaining, decentralized ammonia production hubs, converting steel- and fiber-free rubber chips (5–25 mm) and hydrocarbon off-gases into commercial-grade NH3 on-site.
How the HPDD + ACR + VCD Platform Produces Circular Ammonia
1. Mild Hydrogen Liberation & Carbon Recovery (ACR + 230 °C ITS):
Instead of high-emission thermal gasification or natural gas reforming, clean steel- and fiber-free tyre rubber chips (5–25 mm) are processed through our +600 bar hydrostatically pulsed Acoustic Cavitation Reactor (ACR) paired with our unpressurized 230 °C closed-loop siloxane thermal system. Intense cavitation shockwaves cleave polymer and sulfur bonds at mild temperatures (≤ 230 °C), liberating hydrogen-rich gas streams while separating solid carbon into high-grade recovered Carbon Black (rCB).
2. Compact On-Site Nitrogen Capture & NH3 Synthesis Skid:
The purified hydrogen stream is combined with nitrogen (N2) separated directly from ambient air inside a modular, containerized catalytic synthesis loop. Operating continuously at steady state, the synthesis skid converts local waste-derived hydrogen and air into pure ammonia (NH3), eliminating imported fossil feedstock and long-distance chemical transport.
3. Self-Sustaining Power & Heat Core (HPDD on NH3, ΔMass = 0.000 kg):
A fraction of the synthesized NH3 feeds our hermetically sealed, zero-exhaust +600 bar opposed free-piston HPDD power core (~61% net electrical efficiency, frictionless 25-micron gas-curtain seal). Operating inside a 100% closed thermodynamic loop (ΔMass = 0.000 kg), the HPDD core supplies 24/7 off-grid electricity to run your shredders, cracker mills, and air-separation compressors, alongside 230 °C process heat and clean recovered water, leaving surplus circular ammonia ready for direct commercial sale.
Strategic Advantages for Tyre Recyclers & Industrial Off-Takers
- High-Margin Chemical Off-Take: Monetize waste rubber chips and off-gases by producing commercial ammonia for local fertilizer, refrigeration, and industrial markets alongside high-grade rCB.
- Zero Fossil Natural Gas & Zero Stack Emissions: Synthesize clean NH3 from waste rubber and ambient air with zero CO2, NOx, or exhaust emissions.
- 100% Off-Grid Industrial Autonomy: Generate continuous 24/7 electricity for heavy shredding and synthesis equipment without grid instability or diesel backup.