Upgrade Crude Benzol
Upgrading Crude Benzol into High-Purity BTX (Benzene, Toluene & Xylene)
Transform coal-gasification and coking byproducts into chemical-grade aromatics, without acid-washing waste, cooling towers, or stack emissions.
Crude benzol recovered from coal gasification and coking operations represents a high-volume feedstock that is frequently under-monetized. Conventional upgrading into pure Benzene, Toluene, and Xylene (BTX) relies on hazardous sulfuric acid washing (generating toxic acid sludge), expensive high-pressure catalytic hydrotreating, and energy-intensive distillation towers.
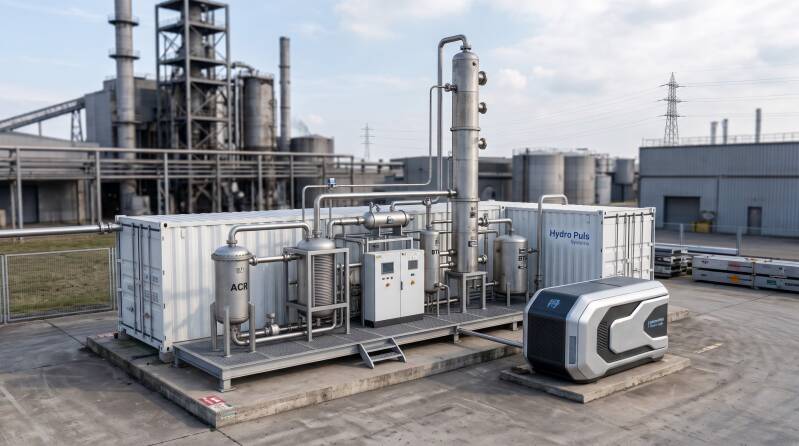
Hydro Puls Systems replaces this heavy refinery train with a compact, modular, closed-loop process architecture.
How the HPDD + ACR + VCD Platform Upgrades Crude Benzol
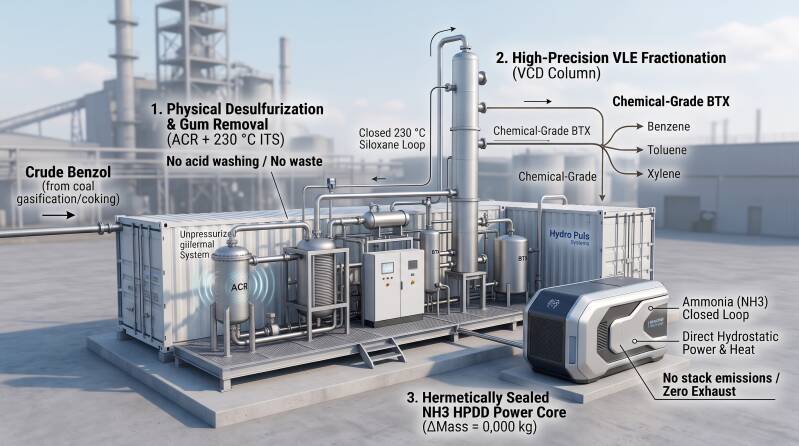
1. Physical Desulfurization & Gum Removal (ACR + 230 °C ITS):
Crude coal-gasification benzol contains stubborn thiophenic sulfur, nitrogen bases, and unstable dienes that polymerize into gums during heating. Routing the feedstock through our Acoustic Cavitation Reactor (ACR) paired with our unpressurized 230 °C Internal Thermal System (ITS) breaks down sulfur compounds and unstable gum-formers physically via cavitation shockwaves—eliminating hazardous acid-washing sludge and catalyst fouling.
2. High-Precision VLE Fractionation (VCD Column):
Separating benzene (80.1 °C), toluene (110.6 °C), and xylenes (138–144 °C) requires tight thermal control. Our Vertical Convective / VLE Column (VCD) leverages cascaded thermal gradients from the closed 230 °C siloxane loop to isolate high-purity, chemical-grade BTX cuts inside compact containerized skids.
3. Hermetically Sealed NH3 HPDD Power Core (ΔMass = 0.000 kg):
The entire upgrading train is powered autonomously by our Hydro Puls Direct-Drive (HPDD) core, operating exclusively on ammonia (NH3) inside a 100% hermetically sealed, zero-exhaust thermodynamic cycle. Driven by our +600 bar opposed free-piston linear architecture with a frictionless 25-micron gas-curtain seal, HPDD delivers direct hydrostatic power for the ACR alongside the exact 230 °C thermal duty for VCD fractionation, with zero stack emissions.
Strategic Benefits for Gasification & Metallurgical Operators
- Unlock High-Margin Chemical Revenue: Upgrade low-value crude benzol on-site into marketable chemical-grade benzene, toluene, and xylene.
- Eliminate Acid Sludge & Heavy OPEX: Purely physical acoustic cavitation and closed-loop thermal management replace chemical scrubbing and steam-heavy columns.
- Modular Containerized Deployment: Repeatable skid-mounted blocks integrate directly into existing coal-gasification and metallurgical plants with minimal water demand.