APPLICATION VERTICALS: ADVANCED BIOFUELS & CIRCULAR HYDROCARBONS
Continuous Upgrading of Pyrolysis Oil into High-Grade SAF Feedstock
In-line hydrodynamic de-polymerization, viscosity reduction, and off-grid process intensification for bio-crude and plastic pyrolysis oils.
Executive Overview
Raw pyrolysis oil—derived from mixed plastic waste, forestry residues, or agricultural biomass—represents a vital feedstock for circular fuels and Sustainable Aviation Fuel (SAF). However, commercial deployment is systematically blocked by downstream processing hurdles: extreme viscosity, high acidity (TAN), thermal instability, micro-emulsified water, and rapid repolymerization (gumming) during storage.
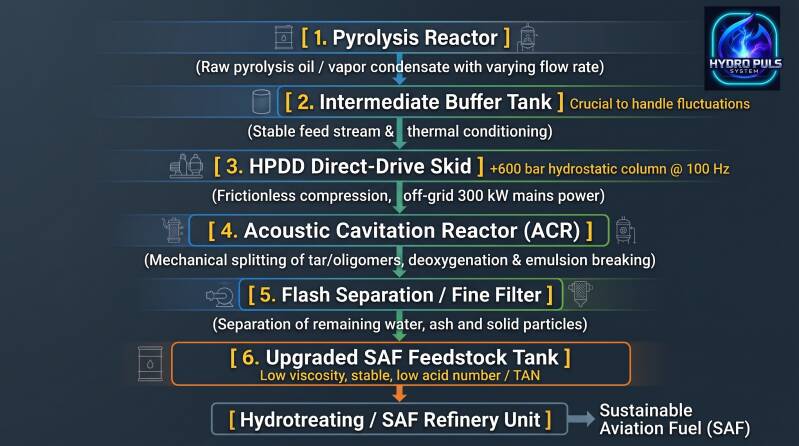
The Hydro Puls Direct-Drive (HPDD) platform, combined with the Acoustic Cavitation Reactor (ACR), replaces conventional, cost-heavy chemical pre-treatments and high-maintenance fossil utility boilers with purely mechanical, continuous process intensification. Directly integrated at the reactor outlet, HPDD-ACR stabilizes, de-ashes, and homogenizes bio-crude into a stable, refinery-ready intermediate.
Key Technical & Operational Capabilities
1. Inline Acoustic Oligomer & Tar Shearing
Mechanical depolymerization without external hydrogen or chemical consumables.
• Microsecond Amide & Hydrocarbon Cleavage: High-energy acoustic cavitation shockwaves break high-molecular waxes, heavy oligomers, and gumming precursors at the molecular scale.
• Permanent Viscosity Drop: Converts refractory, sluggish pyrolysis heavy fractions into a free-flowing fluid at reduced operating temperatures, preventing fouling in transport lines.
• Storage Stabilization: Neutralizes free-radical polymerization mechanisms at the source, preventing viscosity creep and phase separation during transit and intermediate storage.
2. Emulsion Demulsification & Moisture Separation
Physical phase separation without chemical demulsifiers.
• Micro-Cavitation Droplet Coalescence: Ultrasonic and hydrodynamic cavitation fields disrupt the protective surfactant envelopes surrounding micro-emulsified water droplets.
• Dissolved Water Liberation: Coalesced moisture and entrapped organic acids separate efficiently in a downstream polishing stage, substantially reducing the Total Acid Number (TAN).
• Preservation of Caloric Density: Strips excess moisture cleanly without degrading light, energy-dense hydrocarbon fractions.
3. De-Ashing & Mineral Particulate Liberation
Protect downstream catalytic hydrotreaters from premature deactivation.
• Particulate Shearing: Hydrodynamic shear forces dislodge sub-micron ash particles, char dust, and inorganic salts bound within heavy hydrocarbon complexes.
• Extended Catalyst Life: Pre-cleared feedstock meets the stringent particulate and metal thresholds of hydrotreating and co-processing units, eliminating severe catalyst poisoning.
4. Seamless Integration via Intermediate Buffer Architecture
Engineered to withstand fluctuating pyrolysis outputs.
• Supply Equalization: Integrated directly via an inline buffer tank following reactor condensation, absorbing yield and temperature variances without starving high-pressure pumps.
• Continuous +600 bar Column: Delivers uninterrupted hydrostatic pulses through a frictionless 5-micron gas curtain labyrinth seal, completely avoiding seal wear from abrasive bio-oils.
5. 100% Autonomous Off-Grid Operation
Complete utility independence for remote biomass and recycling sites.
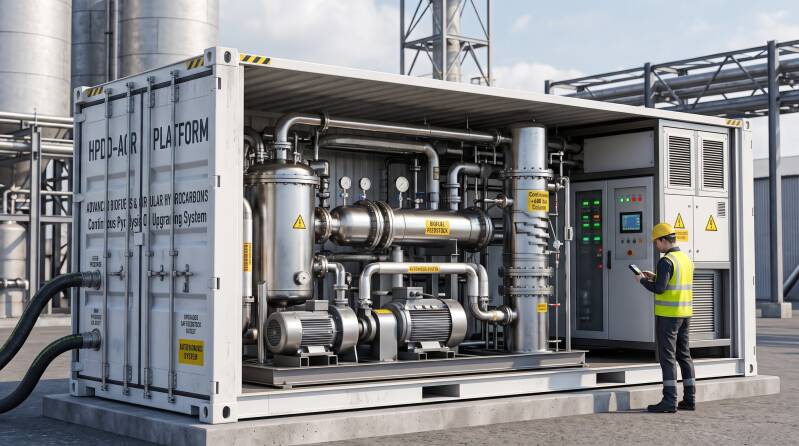
• 300 kW Net Autonomous Power: Each modular 20ft containerized skid generates its own continuous baseline electricity, requiring no grid connection.
• High-Grade Heat Integration (230 °C ITS): Thermal energy recovered from the internal nitrogen cycle provides base heat for feed conditioning and pre-heating, eliminating external fossil fuel boilers.
Upgraded Feedstock Specifications for SAF & Co-Processing
• Kinematic Viscosity: Substantially reduced to ensure pumpability and inline metering.
• Moisture Content: Stripped to refinery-acceptable thresholds for direct catalytic processing.
• Stability: Repolymerization suppressed for extended shelf-life and transport.
• Deployment Model: Standardized 20ft ISO container skids for plug-and-play installation directly at the pyrolysis plant gate.