

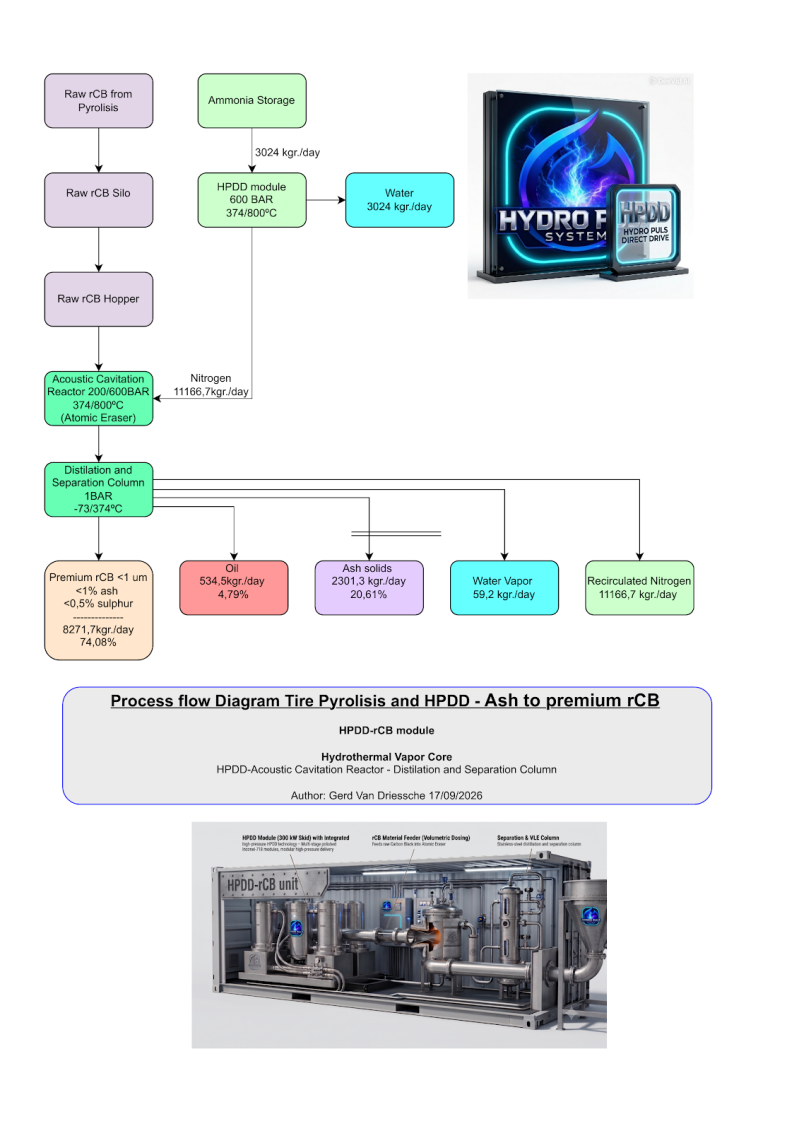
The Process Flow Diagram illustrates the continuous, zero-emission integration of the Hydro Puls Direct-Drive (HPDD) platform with end-of-life tire pyrolysis for the high-yield upcycling of raw Recovered Carbon Black (rCB) into premium technical-grade carbon.
1. Primary Utility & Kinetic Energy Generation (HPDD Module)
- Feedstock Input: The system consumes 3,024 kg/day of ammonia from storage.
- Operating Conditions: Running at 600 bar and 374 to 800 degrees Celsius, the HPDD core cracks and reacts the ammonia without parasitic rotary losses.
-
Direct Fluidic Outputs:
- Produces 11,166.7 kg/day of high-pressure, superheated inert nitrogen gas.
- Co-produces 3,024 kg/day of clean industrial water.
2. Mechanochemical Deconstruction (Acoustic Cavitation Reactor / Atomic Eraser)
- Feedstock Handling: Raw rCB is fed from the pyrolysis stage through a storage silo and volumetric metering hopper directly into the reactor.
- Reaction Kinetics: The 11,166.7 kg/day supersonic nitrogen flow from the HPDD module is injected into the reactor at 200 to 600 bar and 374 to 800 degrees Celsius.
- Matrix Cleaving: Acoustic cavitation deagglomerates the stubborn carbon structure, stripping away residual hydrocarbons and freeing encapsulated inorganic ash without using mechanical grinding mills.
3. Phase Disengagement & Fractionation (Distillation & Separation Column) Operating at 1 bar across a broad temperature range of minus 73 to plus 374 degrees Celsius, the downstream separation column isolates five distinct product streams:
- Premium rCB (8,271.7 kg/day | 74.08%): Sub-micron particles smaller than 1 micrometer with less than 1% ash and less than 0.5% sulfur, ready for high-grade rubber compounding or battery graphite conversion.
- Ash Solids (2,301.3 kg/day | 20.61%): Decoupled mineral and silica ash separated dry for secondary industrial use.
- Oil (534.5 kg/day | 4.79%): Condensed technical oil recovered for chemical recycling or fuel.
- Water Vapor (59.2 kg/day): Residual moisture removed during thermal separation.
- Recirculated Nitrogen (11,166.7 kg/day): Clean carrier gas recovered at the top of the column for closed-loop recirculation back into the system.